Moulded-in traceability: codes and RFID that never peel
The identity layer is usually the first thing to fail. A barcode label is applied after the part is finished, so it sits on the surface as a separate stack of adhesive, ink and substrate.
Why durable identity matters now
Reuse and circular systems are rewriting the specification. The EU Packaging Regulation, effective August 2026, requires reusable packaging to carry information that it is reusable and to guarantee consistent traceability over its life. In medical devices, FDA direct part marking rules require reusable instruments to carry the unique device identifier on the device itself, still legible after reprocessing. Digital product passport platforms such as Utz ID give each reusable container a unique digital identity in a barcode or RFID tag. The common thread across all of them: identity has to survive the entire service life, not just the first journey.
As the packaging industry has put it, the fix is to stop applying a separate identification layer onto the plastic and instead fuse the identity directly into the plastic substrate. That is exactly what in-mould processes do.
How in-mould labelling moves identity below the surface
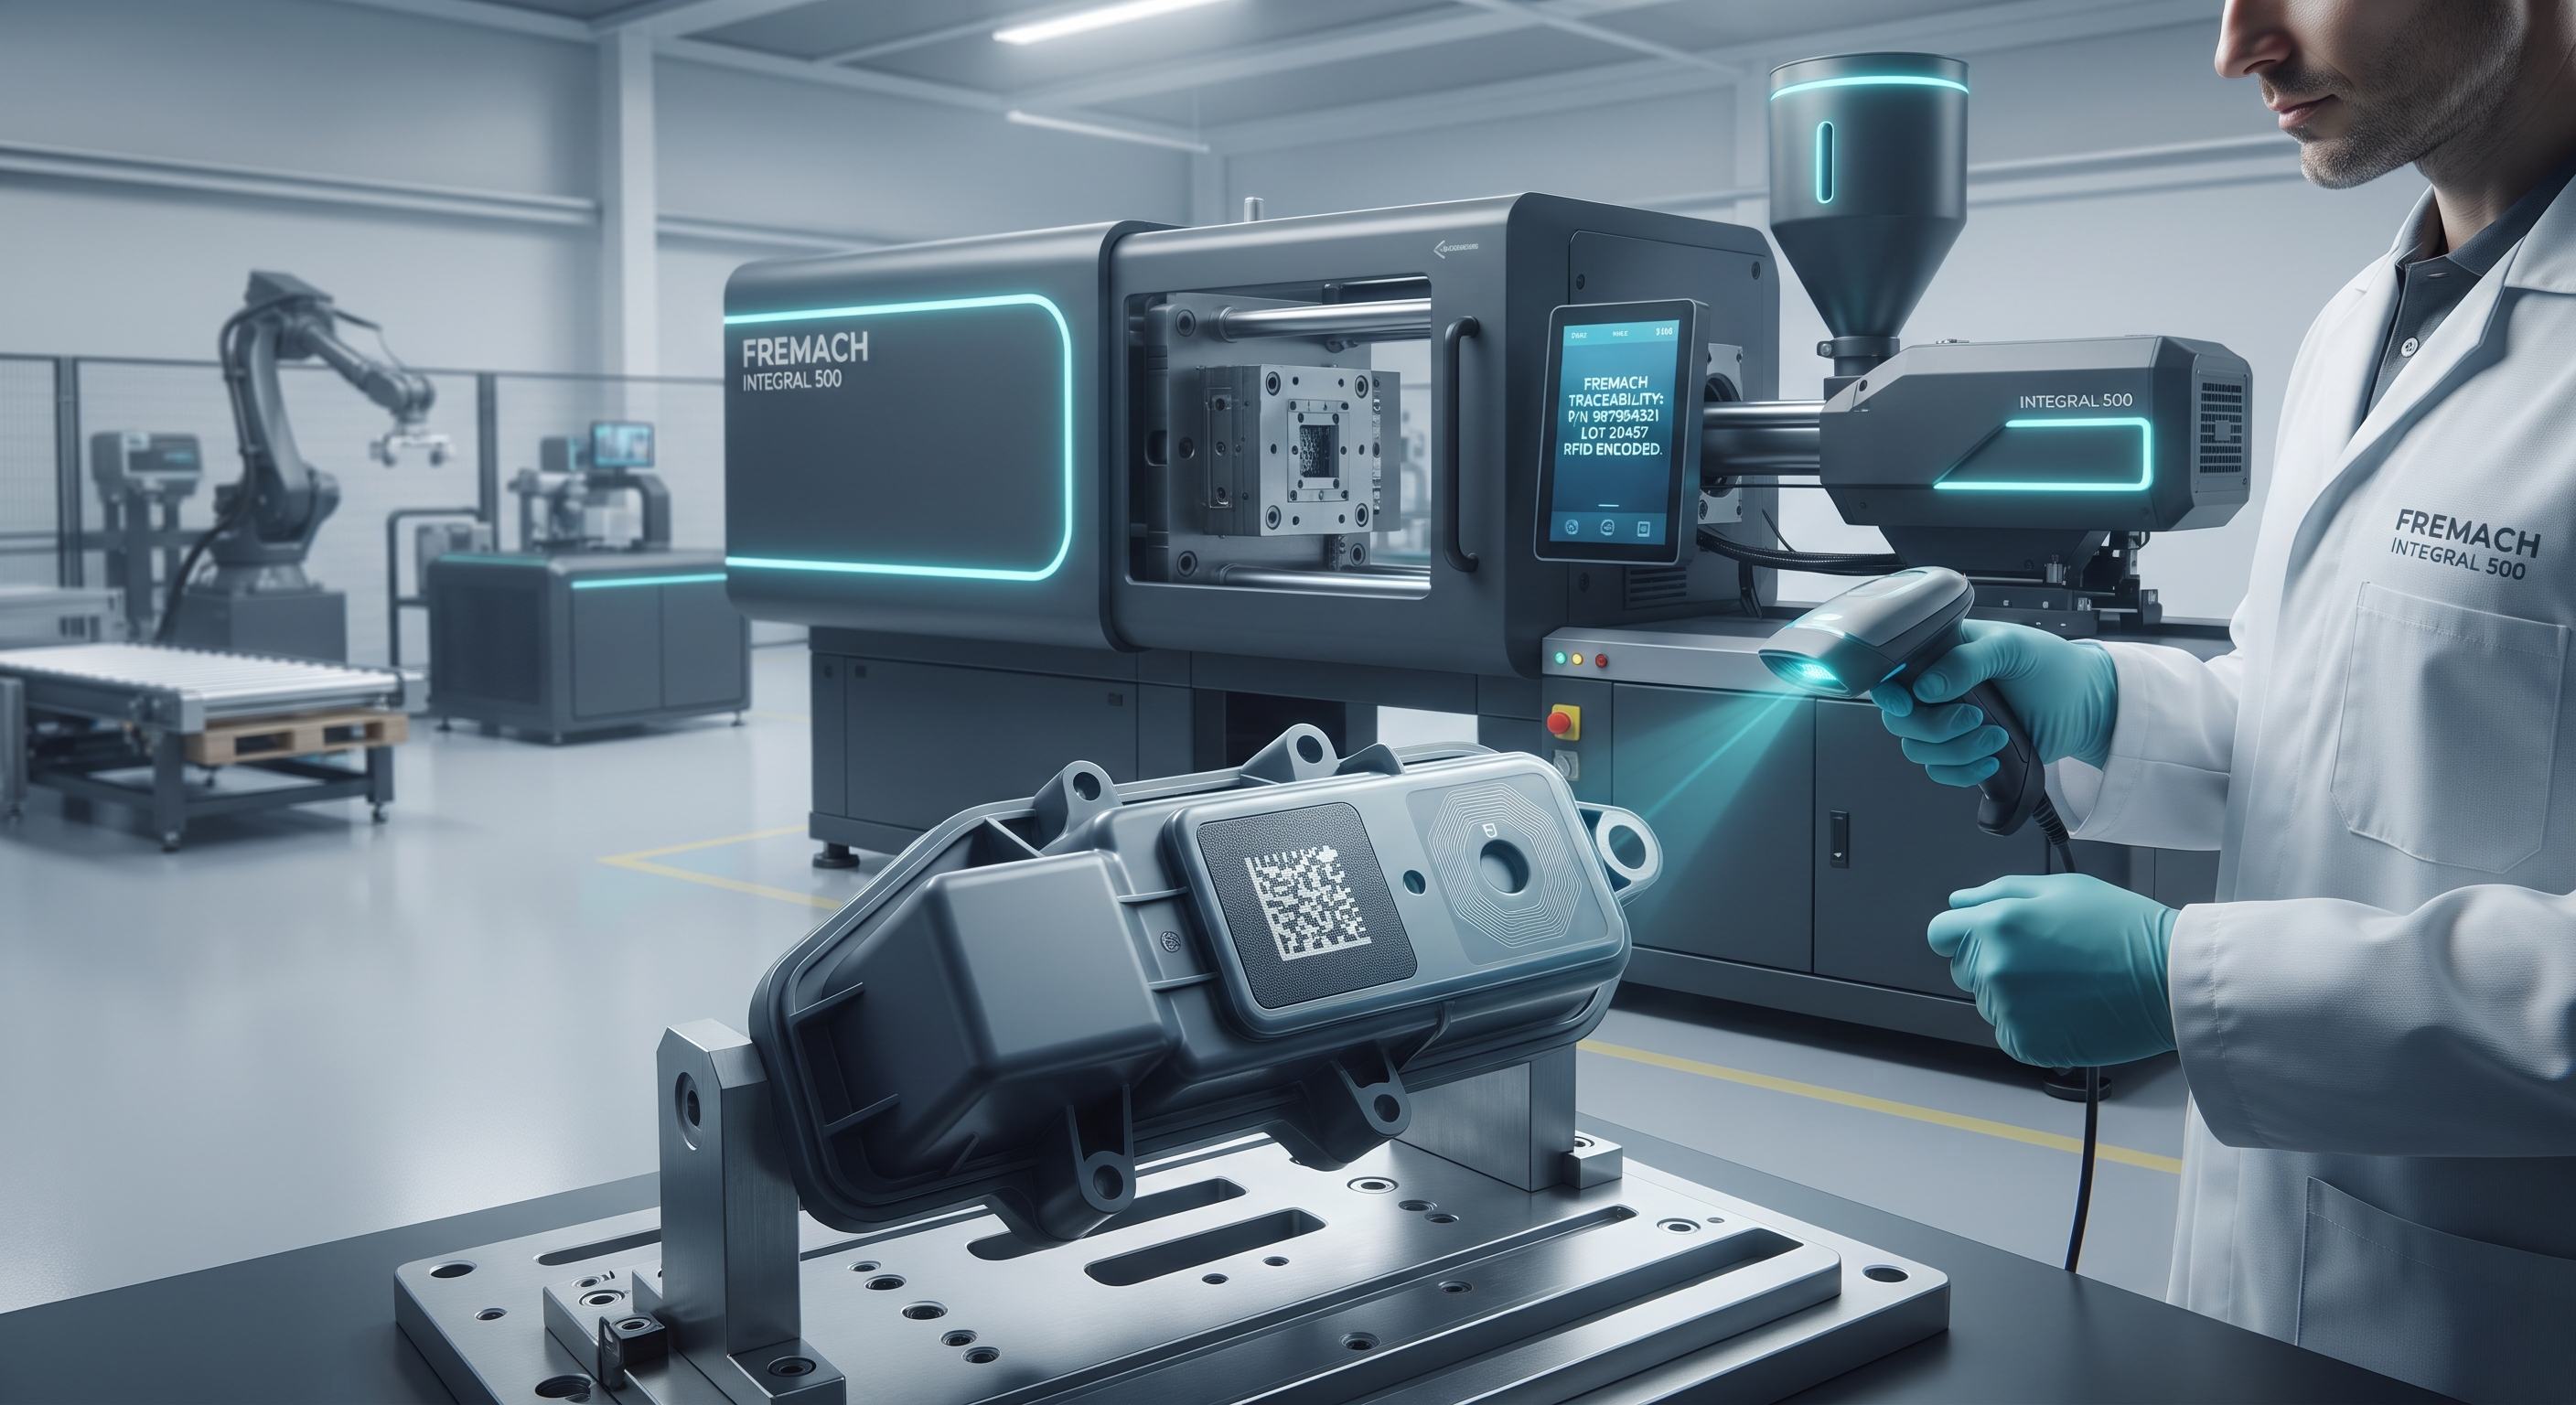
In in-mould labelling (IML), a pre-printed film is placed in the open tool and molten polymer is injected behind it. The film fuses with the substrate and becomes part of the wall, sitting below the surface of wear rather than on top of it. IML is a core decoration process for us, and the same mechanism that carries a logo or a decorated finish can carry a data-matrix code, a QR code or a printed serial number. Because the code is encapsulated in the part, it cannot be peeled, rubbed off or swapped: removing it means destroying the carrier.
RFID takes this further by removing the need for line of sight. Avery Dennison launched an RFID-enabled IML portfolio in July 2025, with UHF inlays engineered to withstand the heat and pressure of injection moulding and to run on standard in-mould labelling equipment and materials. The engineering problem is inlay survival: high-temperature RFID substrates are rated to withstand processing up to 300°C (Avante International), encapsulation in thermoplastic or ceramic shields the working components (Atlas RFID), and in resin transfer moulding temperature-resistant adhesives and coatings hold up to 200°C and 10 bar (PatSnap). Get the inlay specification right and you gain bulk reads, cycle counting and real-time visibility without a visible mark.
One caveat worth designing for: metal detunes antennas. A 2025 patent, WO2025133662A1, describes a compensation antenna to overcome the detuning that metallic components cause. That is directly relevant whenever an RFID carrier shares a part with metal inserts or integrated electronics.
When you do not want a label at all
Sometimes the cleanest identity is no label. Microstructure marking builds the code into the tool itself. imZERT prepares barcode microstructures on tool-steel inserts (1.2344 grade) using a quartz hard-coating, and that texture transfers into almost any plastic and colour during moulding: no ink, no sticker, no engraving and therefore no contamination. Pre-trials show over 100,000 shots without degradation, codes scan from 1mm by 1mm, and there is no added cycle time. ICS Laser Technologies moulds DataMatrix codes directly into parts under its BarCodes in Plastic program, certified to ISO/IEC TR 29158 and AIM DPM-1-2006, with scan capture clocked at 58 to 62 milliseconds in a third-party study by Keyence Canada. Both approaches suit part, mould, cavity and assembly IDs, poka-yoke, and left/right or colour differentiation.
Choosing the carrier
The decision comes down to how the part lives:
Direct-moulded microstructure codes: lowest contamination risk, no consumables, excellent for in-process control, but they need line of sight and good optics.
Printed codes in an IML layer: high contrast, combine full decoration and identity in one operation, protected below the surface.
RFID fused behind IML: no line of sight, bulk and automated reads, best for reuse logistics, provided inlay survival and detuning are engineered in.
This is where our process mix lines up. We run IML as a core decoration process, we mould multi-component (2K/3K) parts, and we integrate electronics and PCBa into decorated components. So the same operation that gives a part its finished, decorated surface can also give it an un-peelable identity: a data-matrix inside the IML layer, an RFID inlay fused behind the decoration, or a microstructure code moulded into a hidden face. Handling decoration and electronics together means we can place the carrier where it both survives and still reads.
If you are developing a reusable container, an industrial housing, a consumer product or any part that has to stay identifiable for its whole life, that identity decision belongs in the part design, not bolted on afterwards. Bring your part or drawing to our engineers and we will work out which carrier fits and how to mould it in.
Talk to our team
Stay in the loop.
Subscribe to our newsletter for new articles, project stories and technology insights. No spam, unsubscribe anytime.
Want to discuss a project?
Bring us a drawing, a target volume, or just a challenge. Our engineers review every brief and respond within two business days.